How Heat Pump Food Dryers Cut Energy Use vs Conventional Hot-Air
Energy is one of the largest operating costs in commercial fruit and food drying. For export-oriented plants in humid climates, every kilogram of water removed from mango, banana, pineapple, herbs, seafood, or similar materials has a price tag—on the electricity bill, the fuel invoice, or both.
This guide explains heat pump food dryer energy saving in practical buyer language. It compares closed-loop heat recovery with conventional hot-air exhaust loss, lists the questions you should ask about kWh per kilogram of water removed, and outlines when a Soft cost-recovery framework is useful for export plants—without inventing exact savings percentages, guaranteed factory kWh figures, or named customer return-on-investment stories.
Soft note: numbers below are mechanism explanations, published literature bands, or public site positioning. They are not Airtek performance guarantees for every product, climate, or loading pattern. Plant-specific energy must be estimated from your wet infeed, target moisture, and local tariffs.
Scope lock: this article is about industrial / commercial food dehydrators, not household laundry heat-pump dryers. Keep food in your search and RFQ language.
What “heat pump dryer energy saving” means (buyer definition)
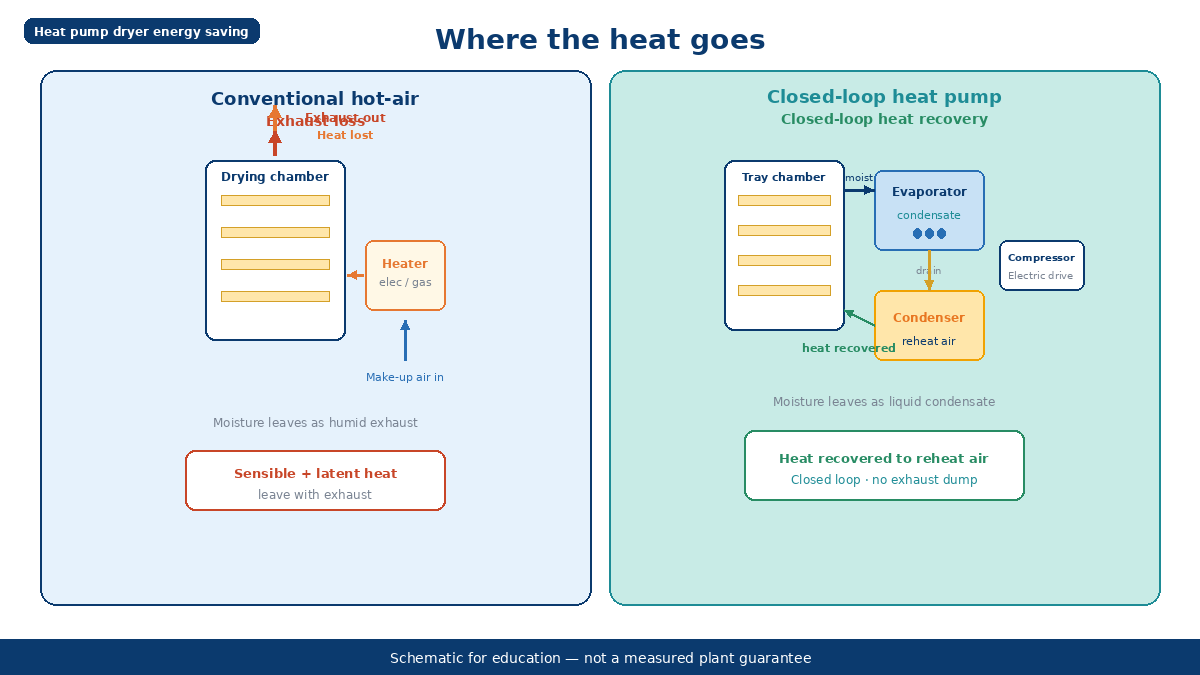
Heat pump dryer energy saving refers to lowering the energy needed per kilogram of water removed by using a closed-loop heat pump food dryer instead of venting heat with exhaust. In a typical closed-loop design, moist air from the drying chamber meets a cold evaporator; water condenses and drains as liquid, while the refrigeration cycle moves recovered heat to a condenser that reheats the air before it returns to the product. Moisture leaves as condensate, not as a full humid exhaust stream.
For commercial fruit and food drying, this mechanism usually improves energy per kg of water removed versus simple hot-air or direct-electric dryers—especially on high-moisture loads in humid climates. Exact kWh, SMER, and any cost-recovery discussion depend on crop, loading, climate, and local tariffs; treat marketing multiples as conversation starters, not contract guarantees.
Airtek builds industrial / commercial heat pump food dehydrators for export-oriented plants. Ask for a project estimate using your wet infeed, target moisture, and electricity price. Machine navigation: heat pump food dryer machine hub.
Why “Energy Per Kilogram of Water Removed” Beats Vague “Efficiency” Claims
Dryer sales conversations often jump straight to “how many times more efficient.” That phrase is easy to say and hard to verify.
What actually drives your operating cost is simpler:
- How much water you must remove (mass balance from initial to final moisture).
- How much useful energy the dryer delivers per unit of electricity (or fuel) consumed.
- How much of that energy is dumped outdoors with exhaust air instead of being reused.
A commercial heat pump food dryer is designed around the second and third points: recover latent heat from condensation, reheat the drying air, and keep temperature and humidity under control inside a relatively closed chamber.
Before you compare quotes, ask vendors to talk in kWh per kg of water removed (or the inverse, kg water per kWh—often called SMER). That metric travels better across fruit types than a single “efficiency multiplier.”
How a conventional hot-air (or direct-electric) dryer typically spends energy
In many open or semi-open hot-air systems:
- Air is heated with electric elements, steam coils, gas, or coal-fired heat.
- Moist air leaves the chamber as exhaust.
- Make-up air is drawn in from outdoors and heated again.
That exhaust stream carries away both sensible heat (hot air) and latent heat (water vapor). In humid tropics, outdoor air is already moist, so you may need high exhaust rates just to keep drying force—burning more fuel or electricity to reheat the replacement air.
Direct electric heating is especially transparent: almost every kilowatt-hour of electricity becomes heat at roughly 1:1. Useful for small labs; expensive for continuous multi-tonne water removal.
How a closed-loop heat pump dryer recovers heat
A typical closed-loop heat pump dryer keeps most of the drying air circulating between the chamber and the heat-pump unit:
- Warm, relatively dry air enters the drying chamber and picks up moisture from the product.
- Moist air returns to the evaporator, where it is cooled below the dew point.
- Water condenses and drains out of the system as liquid condensate—not as steam dumped outdoors.
- The refrigerant circuit moves that recovered heat to the condenser, which reheats the now-drier air before it returns to the trays.
In short: moisture leaves as condensate; a large share of the latent heat that evaporated the water is recycled into the next pass of drying air. The compressor still consumes electricity, and systems often need a way to reject surplus heat—but you are no longer throwing the entire humid exhaust stream away on every cycle.
| Dimension | Conventional hot air / direct electric (typical) | Closed-loop heat pump dryer (typical) |
|---|---|---|
| Moisture removal path | Exhaust humid air outdoors | Condense water on evaporator; drain condensate |
| Heat in exhaust | Sensible + latent heat largely lost | Latent heat largely recovered for reheat |
| Make-up air | Often large outdoor intake | Minimal once loop is sealed (design-dependent) |
| Humidity control | Strongly tied to exhaust rate & weather | Temperature and RH can be programmed more independently |
| Energy narrative | Heat = fuel/electric almost 1:1 or fuel-fired | Electricity drives a heat pump (COP / SMER direction) |
This is the core of heat pump dryer energy saving: not magic multipliers, but not dumping recoverable heat with the exhaust.
What Buyers Should Ask About kWh per kg Water Removed
Define the metric before you compare quotes
Two related indicators appear in drying literature and vendor talks:
| Metric | Meaning | Why it matters |
|---|---|---|
| SMER (Specific Moisture Extraction Rate) | kg of water removed per kWh of electricity (or energy) input | Higher SMER → more water removed per unit energy |
| Energy intensity | kWh per kg of water removed (the inverse framing) | Easier to multiply by your daily water load for a bill estimate |
| COP (Coefficient of Performance) | Useful heat delivered ÷ electrical work to the compressor (order-of-magnitude heat-pump language) | Explains why heat pumps beat 1:1 electric heaters—but drying COP is not identical to room-heating COP |
Ask every supplier—including Airtek—to clarify:
- Is the figure measured or estimated?
- Over a full batch or only the “easy” constant-rate drying phase?
- For which product, thickness, loading density, and ambient conditions?
- Does it include fans, defrost, and auxiliary heaters, or only the compressor?
Literature context (not Airtek guarantees)
Peer-reviewed reviews of heat pump drying for fruits and vegetables often report SMER bands for HPD systems that sit higher than simple hot-air dryers in classic comparison tables. Published ranges vary widely with crop, temperature, and system design—treat them as order-of-magnitude background, not a purchase contract number.
Airtek’s public site may describe heat pump dryers as substantially more energy-efficient than direct electric heating in Soft marketing / order-of-magnitude language. Treat any multiple as a conversation starter, not a measured plant guarantee. Validate with a project estimate from your water mass balance and local tariff.
A practical calculation skeleton (fill with your numbers)
- Lock wet infeed mass and moisture (wet basis).
- Lock target moisture.
- Estimate water to remove from mass balance.
- Ask for an estimated kWh per kg water (or SMER) under your loading and climate assumptions.
- Multiply daily energy ≈ water removed × (kWh/kg water).
- Multiply by local electricity tariff and expected operating hours / load factor.
Only after those steps does a Soft cost-recovery discussion become meaningful. Skipping straight to “we save X%” without a water-mass balance is how plants buy the wrong story.
When a Soft Cost-Recovery Framework Matters for Export Plants
Not every processor needs a formal spreadsheet on day one. A Soft framework becomes useful when several of the following are true: high daily water removal; electric heating or expensive grid power; humid tropical sites; export quality + schedule pressure; fuel / emission constraints; multi-shift / rainy-season continuity.
Situations where the talk can wait: you are still defining the SKU and target moisture; throughput is a pilot line with uncertain utilization; the dominant decision driver is hygiene or buyer audit—energy is secondary but still worth estimating later.
Rules for trustworthy use: baseline must be explicit; annual energy needs your water load × estimated kWh/kg delta × tariff × utilization; include maintenance honestly; do not treat marketing multiples as contractual savings; do not invent return-on-investment percentages or fixed recovery years.
CapEx vs OpEx Soft reading (sibling gold): Heat pump vs electric resistance food dryer TCO.
Side-by-Side: What Changes on the Factory Floor
| Topic | Conventional hot-air / direct electric | Closed-loop heat pump |
|---|---|---|
| Energy flow | Heat in → much of it out with exhaust | Heat in (compressor + fans) → large share recycled via condensation reheat |
| Weather dependence | Exhaust systems feel outdoor humidity | Drying RH more chamber-controlled |
| Product quality story | High T or unstable RH can darken sensitive fruit | Milder programmed T/RH often favored for color and aroma (still product-specific) |
| CapEx | Often lower for simple cabinets | Often higher upfront |
| OpEx direction | Higher when electricity or fuel is costly | Usually lower energy per kg water removed—magnitude site-specific |
| Best fit | Small scale, cheap fuel, low utilization | Medium–large water loads, export quality, humid climates, multi-product tray plants |
Buyer Checklist: Energy Questions to Put in Your RFQ
- Product & geometry — type, slice thickness, tray loading target.
- Moisture basis — initial / final, wet vs dry basis stated clearly.
- Water mass per batch / day — calculated water removed, not only “dryer capacity kg.”
- Energy metric — estimated SMER or kWh per kg water, with inclusions (fans, defrost, auxiliaries).
- Ambient design point — dry-bulb / RH for the installation site.
- Electrical supply — voltage, frequency, available kW.
- Baseline for comparison — what dryer you run today (or would buy instead).
- Utilization — batches per day, days per year, rainy-season schedule.
- Quality constraints — max product temperature, color specs, additive rules.
- Service — warranty scope, spare parts lead time, local support expectations.
Low-temperature / gentle process questions (different angle from this energy frame): Low-heat food dehydrator process FAQ.
FAQ — Heat pump food dryer energy saving
Q1. How do heat pump food dryers save energy compared with conventional hot-air dryers?
A. Conventional hot-air systems often dump sensible and latent heat with moist exhaust and then reheat outdoor make-up air. A closed-loop heat pump dryer condenses moisture on the evaporator and recycles much of that heat to rewarm chamber air. The practical buyer metric is kWh per kg of water removed (or SMER)—not a single vague “efficiency multiplier.”
Q2. What is SMER, and why should I ask for it in an RFQ?
A. SMER (Specific Moisture Extraction Rate) is kilograms of water removed per kWh of energy input. The inverse framing—kWh per kg of water—is easy to multiply by your daily water load and local tariff. Ask whether the figure is measured or estimated, for which product and loading, over a full batch, and whether fans, defrost, and auxiliaries are included.
Q3. Are website “times more efficient” claims guaranteed plant results?
A. No. Public Soft marketing language is a conversation starter, not a measured guarantee for every food, climate, or loading pattern. Validate with a project energy discussion using your mass balance and tariff.
Q4. When does a Soft cost-recovery framework matter for an export food plant?
A. When daily water removal is large, electricity or fuel is costly, the site is humid, and you need weather-independent quality and schedule. Use incremental CapEx ÷ (annual energy cost saved + other verified OPEX deltas)—and skip “we save X%” claims that omit wet infeed, target moisture, and utilization. Do not invent fixed cost-recovery years.
Q5. What should I send Airtek to discuss energy realistically?
A. Send crop and form, wet kg per batch or day, initial and final moisture (state wet vs dry basis), slice thickness / loading intent, site power (V/phase), ambient design point, and your baseline dryer. Use the product inquiry form.
Soft Takeaway for Commercial Buyers
Heat pump food dryer energy saving is real in mechanism terms: closed-loop systems recover condensation heat instead of venting it with exhaust. That usually improves energy per kilogram of water removed versus simple hot-air or direct-electric designs—especially on high-moisture loads in humid climates.
What is not automatic: a fixed “save X%” for every SKU; a universal recovery year that ignores tariff and utilization; treating website marketing multiples as contract guarantees.
Soft next reads (do not paste hard numbers between posts):
- Machine hub: Heat pump food dryer machine
- CapEx / OpEx Soft: Heat pump vs electric resistance TCO
- Architecture Soft: Batch vs continuous heat pump dryer
- Differentiator Soft: Heat pump food dehydrator advantages
- Process Soft: Low-heat food dehydrator process FAQ
Next step: Request a project estimate with product type, wet batch size, moisture targets, and site power conditions.