 English
 Arabic
 Chinese (Simplified)
 Dutch
 French
 German
 Italian
 Portuguese
 Russian
 Spanish
Bananas are among the world’s most produced fruits—and a large share of surplus fruit never reaches distant fresh markets. For processors in Asia, Latin America, Africa, and beyond, turning ripe or green bananas into dehydrated chips, fruit pieces, or flour is a practical way to cut waste, extend shelf life, and add value.
This guide focuses on commercial banana chips drying and related dried-banana products using a heat pump banana dryer. It covers where bananas come from, moisture targets, slices versus halves versus whole fruit, process cautions (including browning), whether heat pump drying is feasible, a transparent yield range from 1 tonne of fresh fruit, and why heat pump systems often outperform sun drying and simple hot-air setups.
Soft note for buyers: figures below are industry and literature ranges under stated assumptions—not guaranteed factory outputs. Final moisture specs should follow your target market’s buyer requirements.
Global Banana Origins: Fresh Export vs Local Processing
According to FAOSTAT-based summaries for 2024, world banana production is on the order of ~139 million tonnes. Approximate leading producers include:
| Rank | Country | Approx. production (Mt) |
|---|---|---|
| 1 | India | ~37.6 |
| 2 | China | ~11.8 |
| 3 | Indonesia | ~9.3 |
| 4 | Ecuador | ~7.6 |
| 5 | Brazil | ~7.0 |
| — | Also significant | Nigeria, Philippines, Angola, and others across Africa and Latin America |
Fresh trade and domestic use differ sharply by country. India and China are huge producers but consume most fruit domestically. Ecuador remains a leading fresh-export powerhouse (export-value share often cited around a quarter of global trade), alongside other Latin American exporters and the Philippines.
Processing narrative (chips, dried banana, flour): drying industries typically grow where there is surplus fruit, local snack demand, or export of value-added products—India, Southeast Asia, West Africa, and parts of Latin America all have established fruit-drying stories. Ripe dessert bananas (e.g. Cavendish types) tend toward sweet chips and “banana raisin / banana-passa” styles; green cooking bananas / plantains more often go into starch-rich flour.
There is no single authoritative public table for the share of acreage “dedicated to drying” by country. Treat processing as a surplus + local value-addition story—not a fixed global percentage.
Moisture: Starting Fresh, Ending Shelf-Stable
Typical initial moisture
Fresh ripe banana pulp commonly sits around 74–80% moisture (wet basis) before drying (literature often clusters near 73–80%, depending on cultivar and ripeness). Green banana slices can run slightly higher (roughly 79–83% wb in some Indian cultivar studies). Industry process pages sometimes quote ~70–75%; ripeness and variety explain much of that spread.
Target moisture by product type
Do not mix product categories:
| Product | Typical target moisture % (wb) | Notes |
|---|---|---|
| Dehydrated sweet chips / snack slices | Often ~10–15% (industry pages commonly cite 12–15%; lab trials often dry toward ~10%) | Too wet → soft / leather-like and storage risk; too dry → brittle packaging breakage |
| Green banana flour | Often ~5–7% | Favors milling and storage |
| Banana powder | Often ~3–5% (after spray/drum routes, then further drying) | High-solubility uses |
| Fried banana chips | Commercial specs may demand very low moisture (sometimes near ~4–5% order of magnitude) | Oil-containing—a different product from dehydrated chips |
For microbial stability, water activity Aw below ~0.60 is a widely used practical threshold. Heat-pump-assisted drying studies on banana slices have reported Aw near ~0.58 at a 45°C end condition in closed-loop systems—useful as research context, not a universal packing rule. Export buyers usually care about low moisture + low Aw + moisture-barrier packaging.
Legal or buyer moisture caps for dehydrated banana chips vary by destination market. Do not apply fried-crisp standards (for example regional “banana crisps” specs written for frying) to heat-pump / hot-air dehydrated slices—confirm the buyer’s dehydrated-product spec for your destination market.
Slices vs Halves vs Whole Fruit
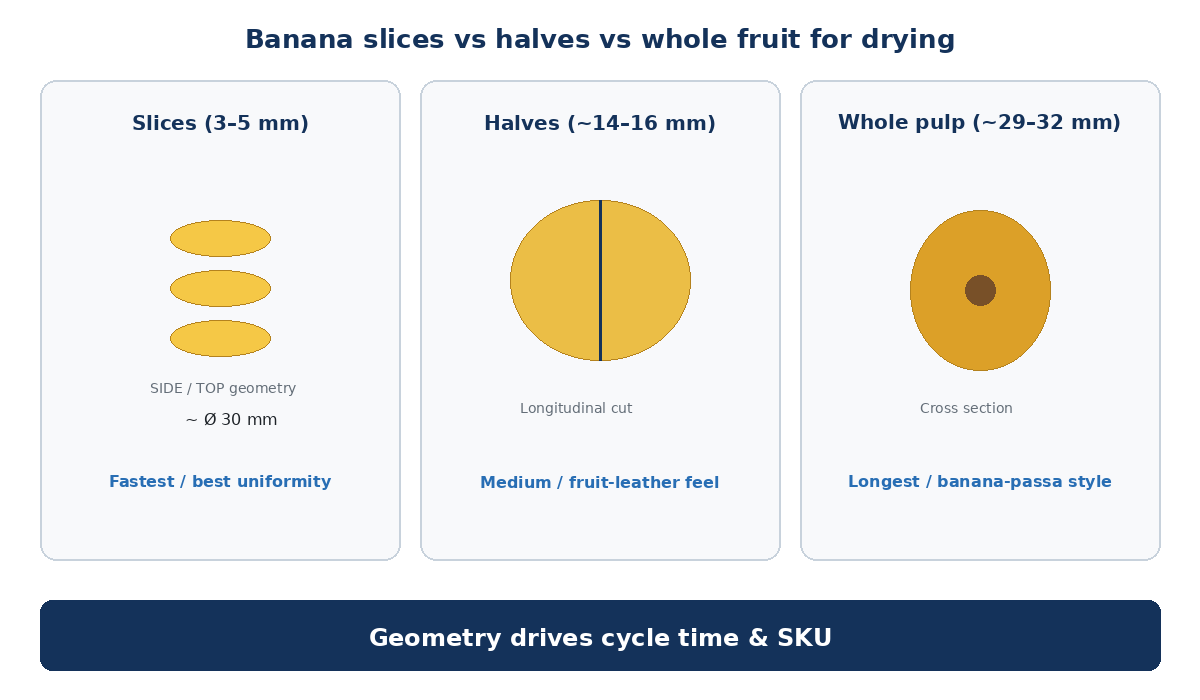
Geometry drives drying time, uniformity, and SKU style. Brazilian convection-drying work on ripe Nanica bananas (slice thicknesses including 5 / 10 / 20 mm, halves ~14–16 mm, whole pulp ~29–32 mm; 35–70°C) illustrates how long cycles can stretch—from roughly 4 hours for thin pieces up toward tens of hours for whole fruit under mild conditions.
| Form | Typical geometry | Time & uniformity | Texture / look | Commercial fit |
|---|---|---|---|---|
| Slices | Often 2–10 mm (snack chips frequently 3–5 mm) | Fastest; short diffusion path; best batch uniformity | Controllable color and crisp/chewy balance | Mainstream dehydrated chips, snacks, re-milling for powder; best tray utilization |
| Halves | Longitudinal cut ~14–16 mm equivalent | Medium; core dries slower than thin slices | More “fruit leather / dried fruit” feel if stopped early | Differentiated dried fruit SKUs, bakery inclusions |
| Whole | Whole pulp ~29–32 mm | Longest; large internal gradients (dry outside / wet inside risk) | Traditional banana raisin / banana-passa style—darker, denser chew | Specialty dried snacks, confectionery inclusions; lower throughput, higher tray occupancy |
Selection logic: high-throughput export chips → thin-to-medium slices on tray heat-pump lines. Traditional dense dried banana → halves or whole fruit, with tighter ripeness control and patience on cycle time. Whole fruit is rarely ideal for high-turn heat pump lines unless you deliberately sell a slow-dried premium piece.
Drying Cautions Processors Should Plan For
Browning (enzymatic and non-enzymatic)
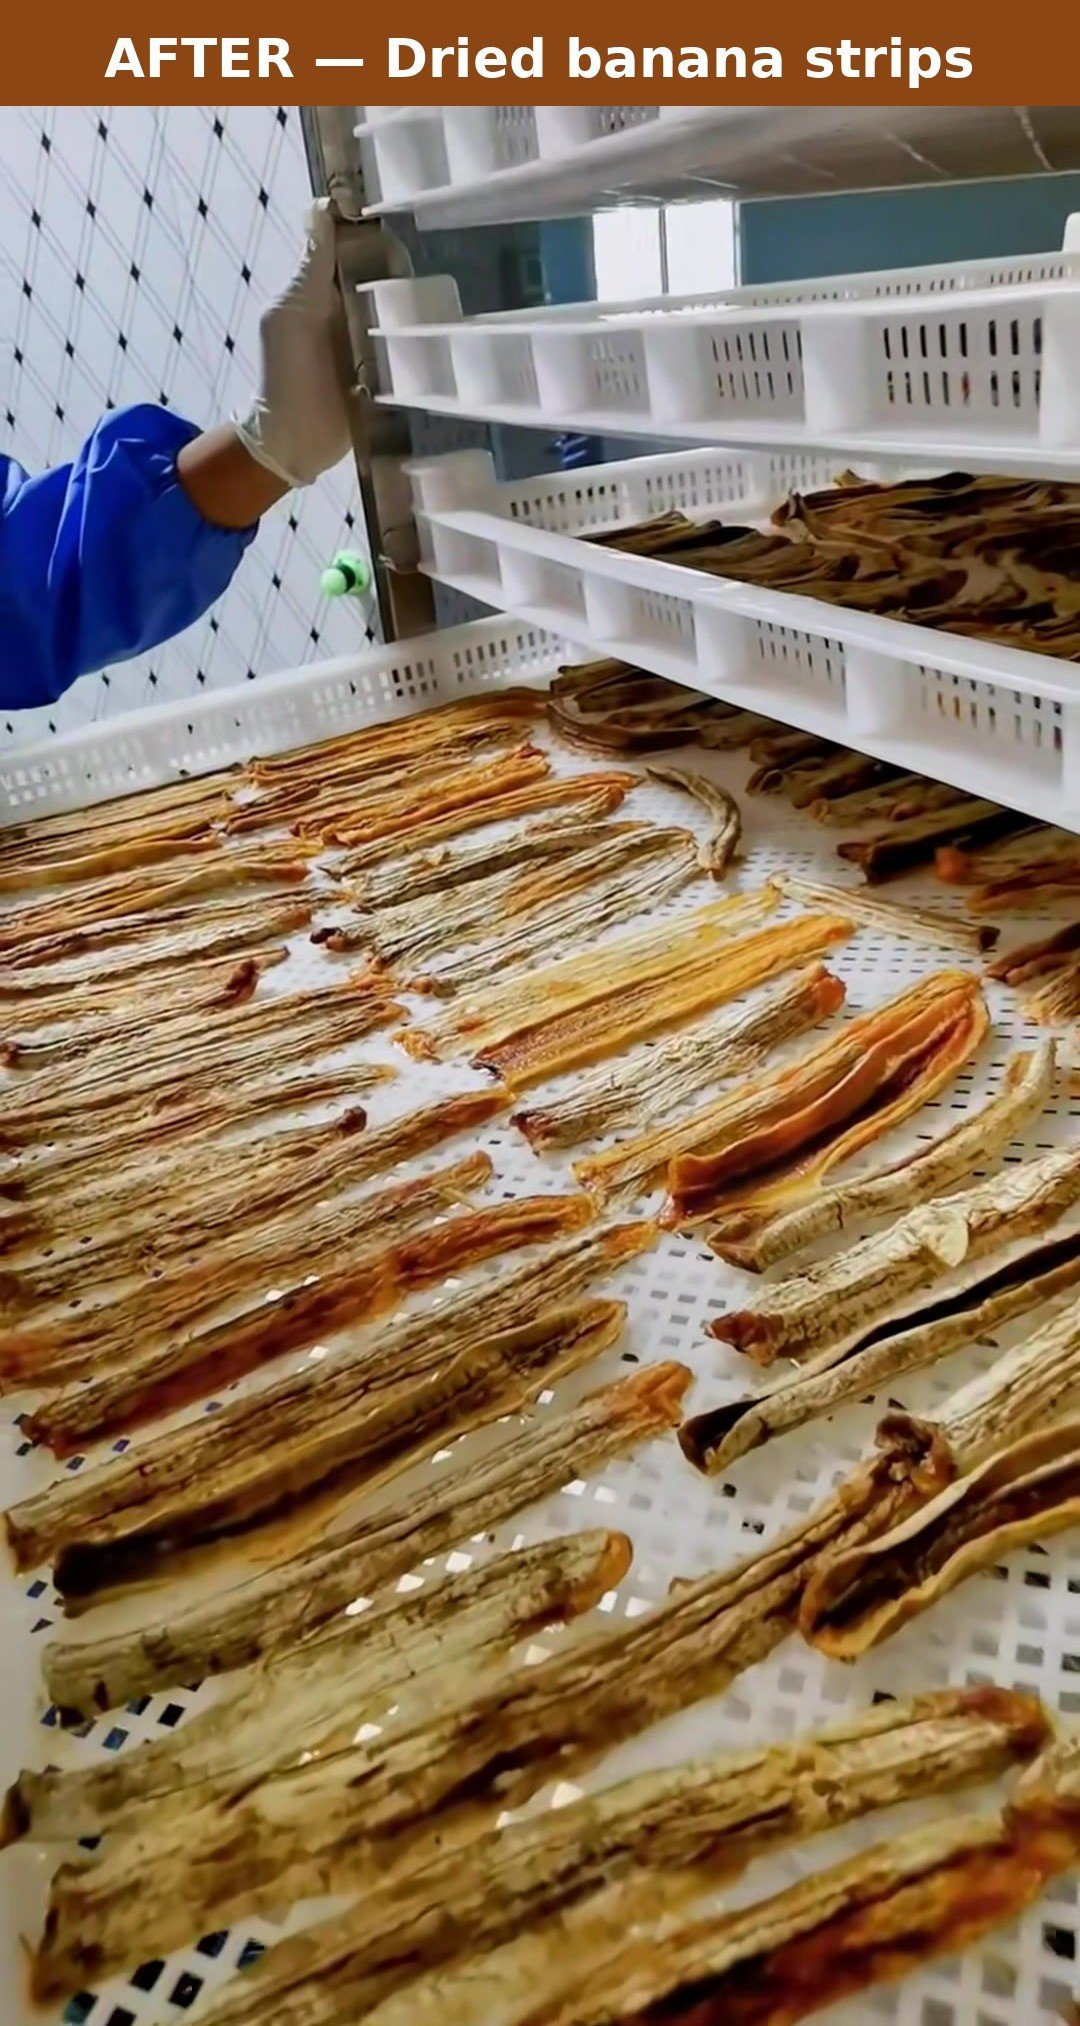
Cutting exposes polyphenol oxidase (PPO) to oxygen—enzymatic browning. Later, high sugar and heat can drive Maillard / caramelization (non-enzymatic) darkening.
Common pretreatments:
- Sulfite dips (e.g. ~0.5% sodium metabisulfite for ~1 minute in some drying-kinetics studies)—effective, but sulfur residue limits apply in some markets.
- Clean-label alternatives: lemon juice, ascorbic acid, or citric acid dips.
A practical heat-pump advantage is the ability to run milder temperature profiles with independently controlled relative humidity, which literature on heat pump fruit drying associates with better color retention and less reliance on heavy sulfiting—when the process is tuned carefully.
Ripeness
- Sweet chips / dried slices: fully yellow but still firm—overripe fruit turns sticky and dark; underripe fruit tastes starchy.
- Green banana flour: process before the fruit turns yellow.
- Very high sugar surfaces stick to trays and clump.
Thickness and tray loading
Uneven thickness means the thickest piece sets the stop time—thin pieces over-dry and shatter. Leave gaps between slices; stacking creates wet cores.
Industry process pages sometimes mention tray loading on the order of ~8–12 kg/m² and air speeds around ~1.5–2.5 m/s. Treat these as generic reference bands only—not Airtek guaranteed setpoints. Actual loading and airflow must be validated on the machine and product.
Tray density and air velocity vary widely by dryer design; treat brochure bands as reference only and confirm by trial on your machine and product—do not copy a brochure number into a purchase contract as a guarantee.
Temperature / humidity curves
Main drying for banana often falls near ~50–70°C. Many quality-focused studies avoid long exposure above ~70°C to limit sugar scorching, dark color, and aroma loss. Closed-loop heat pump trials have also dried banana slices successfully at ~35–45°C—gentler on quality, longer on time.
Late-stage drying should remove bound moisture without case hardening (dry shell, wet center). Driving RH too aggressively can also crust the surface. Heat pumps shine when temperature and humidity can be programmed separately.
Stickiness, mold, and hygiene
Ripe bananas are sticky—use non-stick trays, light release aids, osmotic pretreatment, or a brief surface-dry step before denser loading. Finish moisture that is too high, or packaging that lets humidity back in, invites softening and mold. Cool product before sealing in moisture-barrier packs. Export buyers often ask about GMP / HACCP-style hygiene (wash and peel disciplines belong in the plant design—not only in the dryer).
Dehydrated chips vs fried chips (do not confuse them)
| Fried banana chips | Dehydrated / dried banana chips | |
|---|---|---|
| Process | Thin slices fried in hot oil | Moisture removed by hot air, sun, solar, or heat pump |
| Composition | Absorbs oil | Little or no oil unless coated later |
| Positioning | Traditional crunchy snack | Cleaner-label / fruit-forward stories; natural fit for heat pump energy narratives |
| Equipment story | Fryer lines | Heat pump food dryer territory |
Always specify which product you are quoting capacity and moisture for.
Can You Dry Bananas in a Heat Pump Dryer?
Yes. Peer-reviewed work and industry practice both support heat pump drying of banana slices and related products.
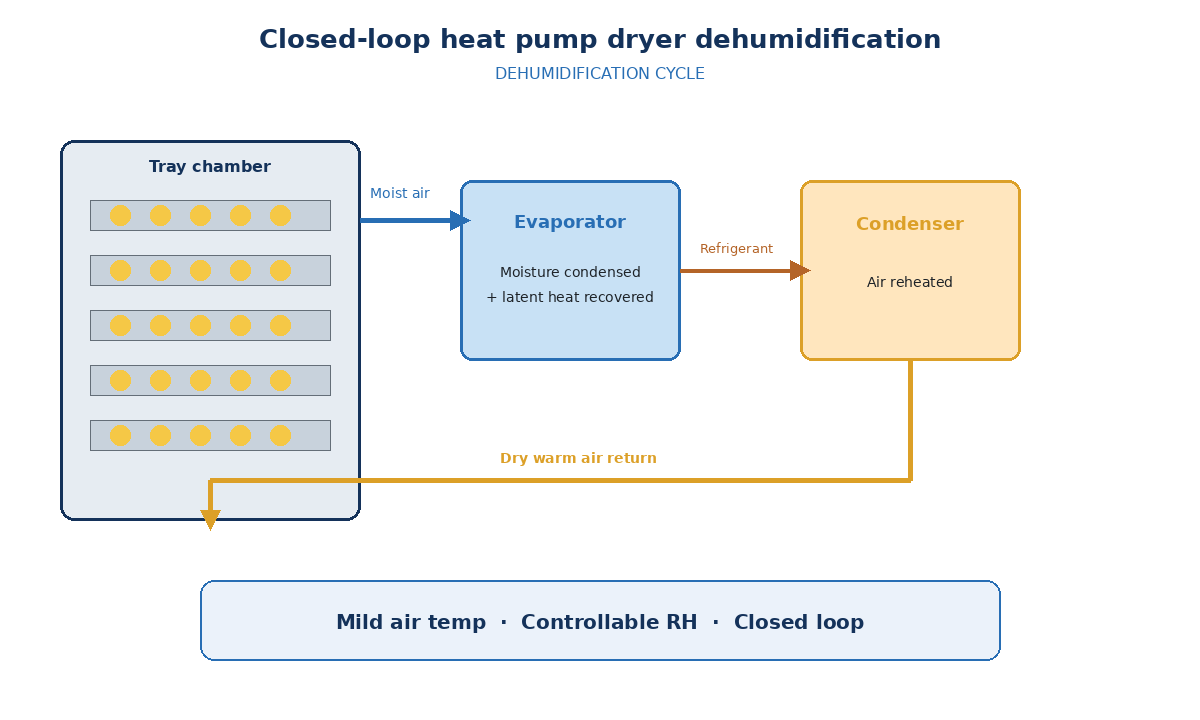
How it works (briefly): In a closed or semi-closed heat pump dryer, moist chamber air passes over an evaporator that condenses moisture and recovers latent heat; the refrigerant then rejects heat at the condenser to rewarm the air before it returns to the trays. For high-moisture fruit like banana, that means useful drying force at relatively mild air temperatures, with less heat and humidity dumped straight outdoors.
Literature anchors (phrased carefully):
- Heat pump–assisted drying systems (HPADS) have dried banana slices in closed loops at about 35 / 40 / 45°C, with thickness strongly affecting time; studies report water activity, SMER, and COP measurements under those conditions (Journal of Food Process Engineering).
- Performance and drying-kinetics modeling of banana slices in heat pump systems appears in renewable-energy research (e.g. Tunçkal & Doymaz, Renewable Energy, 2020).
- Broader reviews of heat pump drying for fruits and vegetables highlight benefits for color, vitamin C, aroma, hygiene, and often higher specific moisture extraction rate (SMER) versus simple hot air—banana is among crops used in case discussions.
For export-oriented processors who care about color, batch repeatability, and energy per kilogram of water removed, a commercial heat pump food dryer is a strong technological fit for banana lines—especially tray dryers sized to your batch wet load.
Yield: How Much Dried Banana from 1 Tonne of Fresh Fruit?
Never treat a single kilogram number as a law of nature. First confirm whether the buyer’s “1 tonne” means whole fruit with peel or already peeled pulp, then lock initial and final moisture assumptions.
Mass-balance idea
W_f = W_pulp × (1 − M_i) / (1 − M_f)
where M_i and M_f are moisture fractions (wet basis) and W_pulp is the mass that actually enters the dryer.
Transparent assumptions (dehydrated sweet chips route)
| Parameter | Conservative | Mid | Optimistic |
|---|---|---|---|
| Whole fruit in | 1000 kg | 1000 kg | 1000 kg |
| Edible pulp after peel | 60% | 65% | 70% |
Initial moisture M_i | 78% | 75% | 73% |
Final moisture M_f | 15% | 12% | 10% |
Peel share in literature often spans roughly 24–47% of fruit weight; mid pulp yields around 60–70% are common planning bands.
Scenario A — 1 tonne = whole fresh bananas (most common inquiry wording)
Moisture removal only (no factory scrap yet):
| Case | Pulp (kg) | Approx. dried slices (kg) |
|---|---|---|
| Conservative | 600 | ~155 |
| Mid | 650 | ~185 |
| Optimistic | 700 | ~210 |
After an additional few percent for crumbs, stickiness, and rejects (plant loss varies by crumbs, stickiness, and sorting rejects), a mid planning band often lands near ~180 kg.
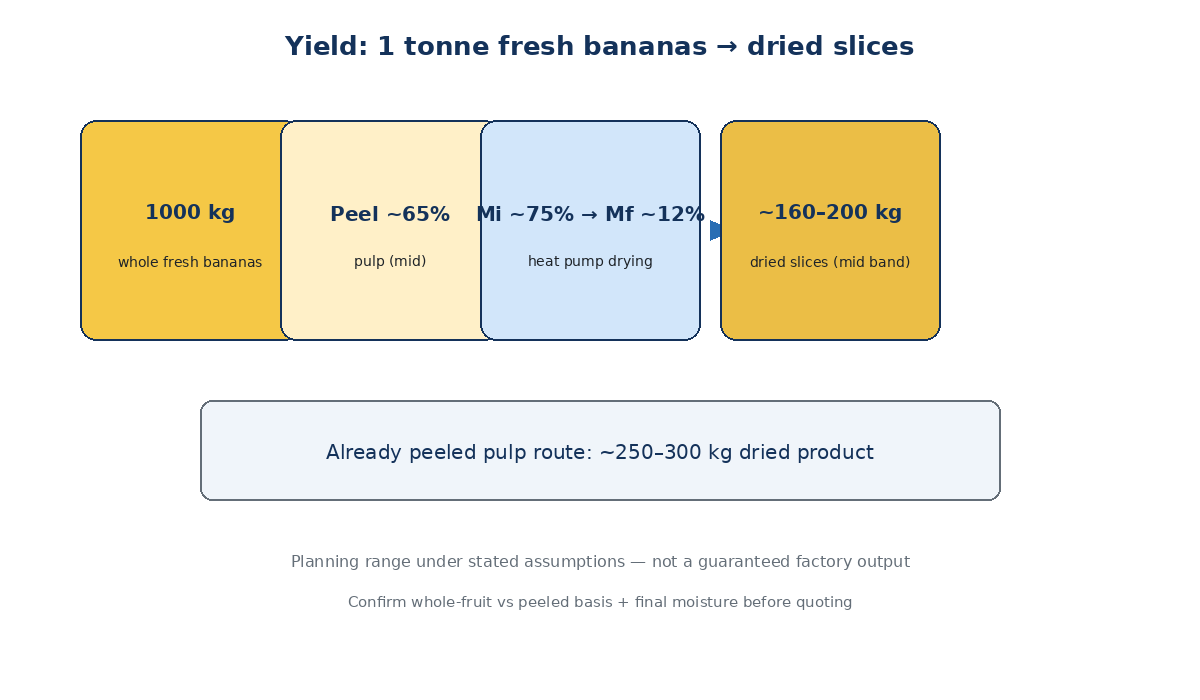
Writer-safe summary: From 1 tonne of whole fresh bananas, after peeling and drying to about 12% moisture, processors typically obtain on the order of 160–200 kg of dried banana slices, depending on peel ratio, ripeness (initial moisture), and final moisture target.
Scenario B — 1 tonne = already peeled pulp
M_i → M_f | Approx. dried product (kg) |
|---|---|
| 78% → 15% | ~259 |
| 75% → 12% | ~284 |
| 73% → 10% | ~300 |
Writer-safe summary: If the 1 tonne is already peeled pulp, expect roughly 250–300 kg of dried product under similar moisture assumptions.
Green banana flour is a different yield story
IITA-style guidance for green banana flour is often framed as about 8–10 kg raw material → 1 kg flour (order of ~100–125 kg flour per tonne of raw fruit, depending on definition of “raw”). Do not reuse sweet-chip yield numbers for flour projects.
Factory loss percentages (crumbs, tray stick, sorting rejects) and destination-market moisture caps vary—use the ranges above as planning bands, not a fixed “guaranteed kg/tonne” claim.
Heat Pump Benefits vs Sun Drying and Conventional Hot Air
| Dimension | vs traditional sun drying | vs coal / direct-fired or simple electric hot air |
|---|---|---|
| Energy | Continuous production regardless of clouds or rain | Recovers condensation latent heat; published HPD SMER bands are often cited roughly ~1.0–4.0 kg water/kWh vs much lower bands for basic hot air in classic comparison tables (review literature; site-specific) |
| Quality | Less dust, insects, scorching, and rain rewetting | Milder T + controllable RH → better color and aroma retention |
| Hygiene / compliance story | Enclosed chamber supports cleaner GMP narratives | No combustion flue contact with food; condensate can be managed |
| Control | Weather-driven batch scatter | Programmable temperature, humidity, and airflow → repeatable batches—critical for export buyers |
| Climate independence | Rainy-season schedules still run | Closed-loop dehumidification maintains low inlet humidity even in humid tropics |
| Operations | Shorter dependence on weather for delivery dates | Lower energy per kg water removed than many straight hot-air systems—exact ROI depends on local electricity tariffs and should be calculated case by case |
One-line takeaway: Heat pump drying helps banana processors run cleaner, more controllable, weather-independent dehydration with better color retention and lower energy per kilogram of water removed than sun drying or simple hot-air systems.
Airtek’s industrial fruit drying machines are built around heat pump technology for fruits and other foods—useful when you need tray-based capacity from small batches up to larger chamber solutions.
Practical Checklist Before You Scale Banana Drying
- Define the SKU: dehydrated chips, halves/whole dried banana, or green banana flour—not fried chips.
- Lock ripeness, peel vs pulp basis, and target moisture (and Aw if your buyer asks).
- Choose geometry (slice thickness first) for the cycle time you can afford.
- Plan pretreatment for browning and stickiness with your market’s additive rules in mind.
- Validate tray loading and airflow on your dryer—do not treat generic industry ranges as guarantees.
- Size the heat pump chamber to your wet infeed per batch, not only to a hoped-for dry-out tonnage.
- Package for moisture barrier after product cool-down.
Talk to Airtek About a Heat Pump Banana Dryer
If you are scoping a commercial banana chips or dried-banana line, share your wet batch size, product form (slices / halves / whole), target moisture, and destination market. The Airtek team can help match a heat pump dehydrator capacity and drying program to your fruit—not a one-size brochure promise.
Next step: send a product inquiry with your raw-material basis (whole fruit or peeled pulp) and daily throughput goal. We will respond with a practical equipment discussion for your plant.
Figures are literature / industry ranges under stated assumptions. Not a substitute for plant trials or destination-market specifications. Brand scope: Airtek / ATK only.